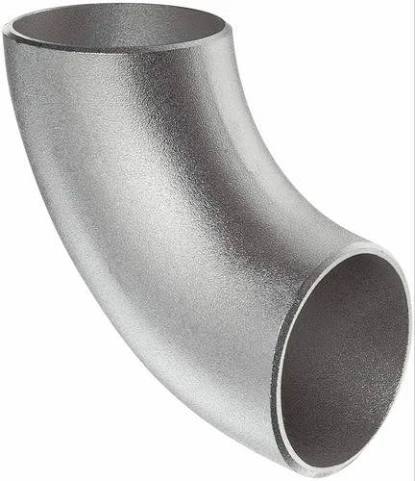
Stainless Steel Socket Weld Elbow Class 3000 to 9000
Stainless steel socket weld elbow for Class 3000, 6000 or 9000 small-bore piping. Compare NPS, Pipe Schedule, socket depth, weld gap, material and WPS.
Description
stainless steel socket weld elbow is a forged fitting for small-bore welded piping. The pipe end is inserted into the socket, and an external fillet weld completes the change in direction. Class alone is not sufficient for ordering. NPS, the mating Pipe Schedule, Material Grade, angle, and the project WPS should also be provided.
Class, NPS, and Pipe Schedule: All Three Fields Are Required
| Inquiry Field | Why It Must Be Provided |
|---|---|
| NPS | Defines the nominal connection size and socket series |
| Class | Identifies the ASME B16.11 fitting series and is not a fixed working-pressure value by itself |
| Pipe Schedule | Affects mating-pipe wall thickness, socket fit, and welding conditions |
| Material Grade | Must match the service medium, design temperature, and project material specification |
| Project WPS | Defines fit-up, gap, filler metal, welding, and inspection requirements |
Four-Step Socket Fit-Up Check
- Check the socket inside diameter, socket depth, and mating-pipe outside diameter, and confirm that the surfaces are free from damage or foreign material.
- Mark the planned insertion position on the pipe end instead of judging socket depth only by feel.
- Reserve the pre-weld gap according to the applicable code and project WPS. A common engineering reference is approximately 1.5 mm (1/16 inch), but the project documents govern.
- Before tack welding, recheck elbow orientation, pipeline centerline, and the gap record, then perform the external Fillet Weld and specified inspection.
When Socket Weld Should Not Be the First Choice
Socket Weld can form a compact permanent welded connection, but the socket geometry leaves an internal step and gap. For systems that are especially sensitive to drainability, cleanliness, or crevice corrosion, the project engineer should compare Socket Weld with Butt Weld.
Where frequent disassembly is required and Threaded fitting is permitted by the project, a threaded connection may be easier to maintain. Larger-bore piping or systems requiring full-penetration butt welds normally require evaluation of Butt Weld. The connection method should follow the system design and project specification.
Factors That Affect Price and Lead Time
- Class and size: Class 3000, 6000, or 9000 and different NPS values require different forging sizes and machining work.
- Material Grade: F304, F304L, F316, F316L, and special materials have different procurement costs.
- Angle and configuration: 90°, 45°, equal-size, or special end patterns affect machining and inventory conditions.
- Inspection documents: MTR, PMI, additional NDE, special marking, and third-party witness requirements must be confirmed separately.
- Order conditions: quantity, lead time, packaging, and destination logistics affect the final quotation.
stainless steel socket weld elbow Specifications
| Parameter | Specification |
|---|---|
| Product Name | Stainless Steel Socket Weld Elbow |
| Product Type | 90 Degree Forged Socket Weld Elbow |
| Elbow Angle | 90°; 45° subject to order confirmation |
| Size Range | NPS 1/8 to NPS 4, common standard range |
| Material | Stainless Steel 304, 304L, 316, 316L |
| Material Standard | ASTM A182 / A182M |
| Material Grade | F304, F304L, F316, F316L |
| Pressure Class | Class 3000, 6000 or 9000 |
| Connection Type | Socket Weld |
| Dimensional Standard | ASME B16.11 |
| Mating Pipe | NPS and Pipe Schedule specified with the order |
| Pre-Weld Gap | Approximately 1.5 mm (1/16 inch), subject to applicable code and project WPS |
| Weld Type | External Fillet Weld, subject to project WPS |
| Manufacturing Type | Forged or Machined from Forged Stock |
| Inspection Items | Visual, Dimensional, Socket and Fit-Up Inspection; additional examination by order |
| Customization | Size, Class, angle, material, marking and inspection documents, subject to technical review |
Frequently Asked Questions (FAQ)
1. Why must both Class and Pipe Schedule be provided?
Class identifies the ASME B16.11 fitting series, while Pipe Schedule describes the wall thickness of the mating pipe. Together they affect socket fit, weld conditions, and project design verification. The actual working pressure should not be determined from the Class designation alone.
2. How should Class 3000, 6000, and 9000 be selected?
Class selection should consider design pressure, design temperature, Material Grade, the mating Pipe Schedule, fluid service category, and the applicable piping code. The inquiry should provide the complete design conditions so technical personnel can verify the stainless steel socket weld elbow and the mating pipe.
More Products